
TLDR
- The UTS EVO CDR Pompe is a magnetic drive metal-running centrifugal pump, certified for project temperatures up to +300 °C.
- The diathermic oil operates between 150 °C and over 300 °C without generating high pressures, but a small leak can cause burns, fires, and soil contamination.
- It magnetic drive eliminates mechanical seals, that is, the most vulnerable point of leakage, and reduces the risk of hot fluid leakage.
- The viscosity of the diathermic oil varies greatly with temperature: the pump must ensure safe cold starts, constant flow rates, and chemical compatibility with the fluid.
- The UTS EVO is designed for continuous use 24/7, in a bare shaft or monobloc configuration, and aims to reduce maintenance and TCO in the medium-long term.
Index
In industrial high-temperature plants, heat control is the most important element of all production. Consequently, thermal fluid management requires highly technological, reliable solutions designed to last over time and minimize operational risks that could be caused by leaks, failures, or malfunctions. In this part of the process industry, the thermal oil pump is therefore one of the most stressed parts of the entire system.It is the component that guarantees the correct circulation of the heat transfer fluid within the circuit, maintaining process stability even under harsh conditions. Furthermore, it operates continuously, at high temperatures, with fluids whose behavior changes depending on operating conditions.
CDR Pompe, thanks to extensive experience in managing critical fluids and complex industrial applications, has developed specific solutions such as UTS EVO, A magnetic drive pump designed to meet the needs of high-temperature industrial sectors.
The choice of the right pump, in fact, involves a series of technical parameters ranging from materials to sealing systems, from environmental safety requirements to the reduction of long-term operating costs.
Chemical and thermal characteristics of diathermic oil
Thermal oil is a heat transfer fluid formulated for heat transfer in closed circuits, generally composed of highly refined mineral bases or synthetic blends with high thermal stability. From a chemical perspective, these oils are designed to resist oxidative and thermal degradation, maintaining their properties even at operating temperatures ranging from 150 °C to over 300 °C, depending on the type. In short, they do not evaporate even at such temperatures.
One of the main characteristics of diathermic oil is indeed the Ability to operate at high temperatures without generating high pressures, unlike water or steam. However, this thermal stability does not eliminate the risks associated with its use. On the contrary, even a small Hot thermal oil leak it can represent a danger: contact with surfaces or people, for example, can cause severe burns, while dispersion into the environment can lead to soil contamination and fire risk, especially if the oil comes into contact with hot surfaces or ignition sources.
From an engineering standpoint, diathermic oil also presents a viscosity strongly dependent on temperature, with high values at cold and lower values at operating temperature. This behavior requires the use of a diathermic oil pump designed to ensure safe startups, constant flow rates, and chemical compatibility with the fluid, preventing degradation, carbonization, or mechanical stress on internal components.
Industrial Applications: Where Reliability is Essential
Diathermy oil is widely used in all industrial sectors where precise temperature control is an essential requirement in production. Even more than in other environments, the choice of diathermic oil pump This directly impacts safety, process quality, and operational continuity.
The main applications include:
-
Chemical industry
Usage in reactors, distillation columns, and heat exchangers, where maintaining constant temperatures is crucial to ensure controlled reactions and products that meet specifications. In these plants, a loss or interruption of flow can compromise the entire production process. -
Pharmaceutical industry
Systems requiring high safety and control standards, with dedicated thermal circuits for dryers, reactors, and continuous production systems. Pump reliability is crucial to prevent contamination and plant shutdowns. -
Food industry
Use for heating tanks, heat exchangers, and process lines, such as in the processing of oils, fats, or high-viscosity products. Here, the diathermic oil pump must ensure hygiene, continuity, and absence of leaks. -
Energy production and industrial thermal plants
Heat accumulation and distribution systems in complex plants where thermal oil is used as the primary fluid for energy transfer.
Main challenges in handling thermal oil
The management of thermal oil presents companies and manufacturers with a series of technical challenges that must be addressed as early as the plant design phase. The choice of a diathermic oil pump inadequate can indeed translate into operational problems, safety risks, and high maintenance costs.
The main critical issues in managing this fluid include:
-
High operating temperatures
The pumps must operate continuously at high temperatures, with meticulously designed materials and components to prevent deformation, loss of tolerances, and degradation of internal components. -
Variable fluid viscosity
Diathermic oil significantly changes viscosity with temperature variation, complicating cold starts and requiring hydraulic solutions capable of adapting to different operating conditions. -
Chemical stability over time
Oil degradation, if not properly managed, can generate residues and deposits that compromise pump efficiency and circuit safety. -
Operational and environmental safety
Any hot oil leaks can cause fires, environmental damage, and risks to personnel, making the adoption of reliable sealing systems and zero-emission solutions crucial. -
Maintenance cost reduction
Plants operating continuously require pumps designed for minimize wear and reduce the frequency of interventions, optimizing the total cost of ownership.
Safety and Risk: Why the Pump is a Critical Component
For all the reasons we've seen, Solutions that eliminate mechanical seals under pressure (and therefore the most vulnerable point of loss) Today they represent a benchmark for high-risk systems. Prevention, early diagnosis, and containment (drains, safety tanks, temperature and level sensors) are mandatory practices alongside the correct choice of diathermic oil pump.
A response from CDR: the UTS EVO diathermic oil pump
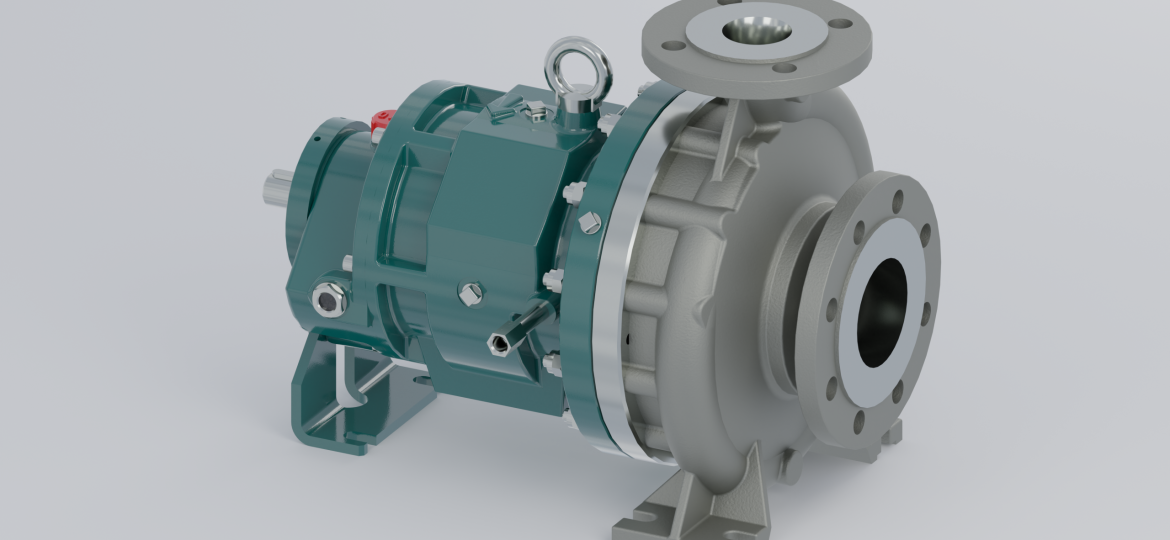
The UTS EVO from CDR Pompe is designed as a magnetic drive centrifugal pump metallica execution that directly addresses the described critical issues. This is a range of pumps designed for continuous 24/7 use, available in bare shaft or close-coupled versions, with selected materials and optimized hydraulic geometries for viscous fluids and high temperatures; the range is certified for design temperatures up to +300 °C.
Use in chemical, pharmaceutical, and food plants It is typical precisely because of the combination of robustness, zero leakage seal, and the possibility of customizing the construction according to process requirements.
UTS EVO: Materials, Magnetic drive, and Performance
The UTS EVO combines in a single solution the key requirements for a diathermic oil pump: AISI materials for the body and key components, internal magnetic core sized to ensure torque even with high-viscosity fluids, and an insulating shell that completely separates the hydraulic circuit from the external environment.
The magnetic drive system eliminates the need for mechanical seals, drastically reducing the risk of fluid temperature loss. The design incorporates internal cooling channels to dissipate heat generated by friction and eddy currents, and a hollow shaft that promotes fluid circulation for the lubrication and cooling of the bushings.
This architecture offers two immediate advantages for the plant manager: firstly, superior operational reliability with less downtime for repairs or maintenance; secondly, Lower maintenance costs and TCO in the medium-to-long term thanks to the reduced number of wear parts and the simplicity of the reconditioning process.
In terms of regulations and safety, the UTS EVO is positioned as a suitable solution when airtight seals and absence of emissions are required., while ensuring competitive hydraulic performance and the ability to customize the product for specific applications.
Performance, maintenance, and return on investment
Using appropriate materials, magnetic levitation, and a design intended for continuous service, The UTS EVO reduces planned and unplanned interventions and lowers overall operating costs. For companies, this translates into lower operational risk, better control of the thermal cycle, and a return on investment that can be evaluated not only on the purchase price but on the entire lifecycle of the pump.
Why choose CDR Pompe
CDR Pompe provides a detailed manual with every centrifugal pump it supplies technical consulting for the correct selection, the composition of materials and system configuration, as well as after-sales services and specific spare parts.
For whom the selection must be made diathermic oil pump, the recommended approach is to evaluate the hydraulic curve, material compatibility, temperature limits, and whether or not magnetic drive and hermetic solutions are available: The UTS EVO provides concrete solutions to these requirements.
Frequently Asked Questions
What is the UTS EVO di thermal oil pump CDR Pompe and for what temperatures is it designed?
The UTS EVO is a metal magnetic drive -running centrifugal pump designed for the circulation of diathermic oil in continuous service 24/7. The range is certified for design temperatures up to +300 °C and is available in a bare shaft or monobloc version, with AISI materials for the body and main components.
Why is it advisable to choose a pump magnetic drive without mechanical seals for diathermy oil?
It is advisable because it magnetic drive eliminates mechanical seals under pressure, which are the most vulnerable point of leakage. With hot oil, even a small leak can cause serious burns, soil contamination and the risk of fire. An insulation shell separates the hydraulic circuit from the external environment and ensures a hermetic seal without emissions.
What are the main difficulties in pumping diathermic oil in a plant industrial?
The main difficulties are high temperatures in continuous operation, very variable viscosity, chemical stability of the fluid over time, operational and environmental safety, and maintenance costs. A degraded oil can form residues and deposits that reduce pump efficiency. At cold temperatures, high viscosity makes starting more complex.
How does the UTS EVO handle the high viscosity of the diathermic oil and the internal cooling?
The UTS EVO uses an internal magnetic core designed to ensure torque even with very viscous fluids and optimized hydraulic geometries for high temperatures. Internal cooling channels dissipate heat generated by friction and parasitic currents. A perforated shaft circulates the fluid to lubricate and cool the bushings.
In which industrial sectors is a diathermic oil pump like the UTS EVO used?
It is used in sectors that require precise temperature control: chemical (reactors, distillation columns, exchangers), pharmaceutical (dryers, reactors, continuous production), in the food industry (heating of tanks and lines for oils, fats and viscous products) and in the energy sector (heat storage and distribution). The typical application of the UTS EVO is in chemical, pharmaceutical and food processing plants.
What parameters should be considered when choosing a diathermic oil pump and how does the UTS EVO reduce costs?
The hydraulic curve, material compatibility, temperature limits, and the presence of sealing solutions should be evaluated magnetic drive. The UTS EVO reduces planned and unscheduled maintenance because it has fewer parts to replace and is easier to repair. The cost should be evaluated over the entire life cycle, not just the purchase price.